Sterility is a critical requirement in pharmaceutical manufacturing, medical device production, and healthcare. Products intended for applications such as injections, eye treatments, and surgical procedures must be free from viable microorganisms that could cause infections or compromise patient safety. Sterility testing plays an essential role in verifying that these products meet the necessary microbiological quality standards before they are released for use.
Understanding how sterility testing works, the methods involved, and the industries that rely on it helps manufacturers maintain product quality, comply with regulatory requirements, and minimize contamination risks.
What Is Sterility Testing?
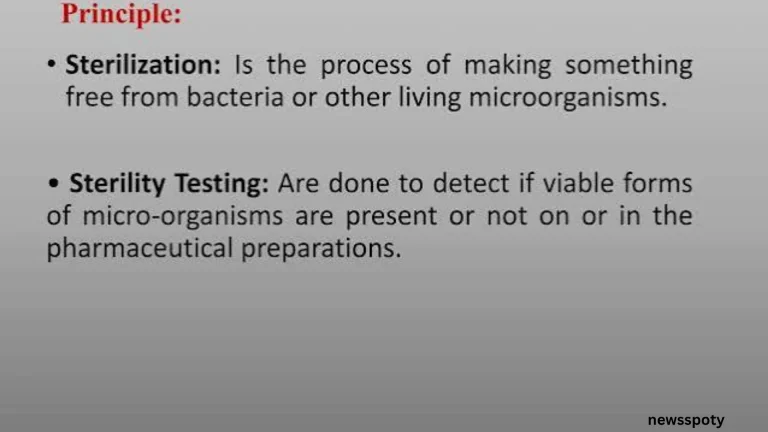
Sterility testing is a microbiological examination performed to determine whether a pharmaceutical product, medical device, or other sterilized material contains viable microorganisms, including bacteria and fungi.
The primary objective is to detect microbial contamination that could pose a risk to patients or affect the safety and quality of a product. Testing is particularly important for products that must remain sterile throughout their intended use, such as injectable medications, ophthalmic preparations, intravenous solutions, and certain medical devices.
Regulatory standards, including the United States Pharmacopeia (USP) Chapter 71 and the European Pharmacopoeia (Ph. Eur.) Chapter 2.6.1, provide established procedures and requirements for sterility testing. These standards help ensure that testing is conducted using appropriate methods and controlled laboratory conditions.
However, sterility testing is not an absolute guarantee that every unit in a manufactured batch is sterile. Since only a sample of the batch is tested, manufacturers must also maintain validated sterilization processes and appropriate contamination-control measures.
Why Is Sterility Testing Important?
Microbial contamination can have serious consequences, particularly when contaminated products enter the bloodstream, come into contact with sensitive tissues, or are used during surgical procedures.
Sterility testing helps manufacturers:
- Protect patient safety: Detect potentially harmful microorganisms before products reach healthcare facilities and patients.
- Maintain product quality: Verify that sterilized products meet established microbiological specifications.
- Meet regulatory requirements: Support compliance with pharmacopeial standards and applicable pharmaceutical regulations.
- Identify contamination risks: Provide information that can support investigations into manufacturing or sterilization failures.
- Support quality assurance: Form part of a broader quality control system that includes environmental monitoring, process validation, and contamination prevention.
Common Methods of Sterility Testing
Two primary methods are commonly used for pharmaceutical sterility testing: membrane filtration and direct inoculation. The appropriate method depends on the product’s characteristics, formulation, and potential interactions with the testing materials.
1. Membrane Filtration Method
Membrane filtration is commonly used for products that can pass through a suitable filter without damaging or obstructing it. During this procedure, a measured quantity of the product is passed through a sterile membrane filter designed to retain microorganisms.
The membrane is then rinsed, when necessary, to remove substances that could inhibit microbial growth. It is subsequently transferred into appropriate culture media to encourage the growth of any microorganisms present.
This method is particularly useful for filterable liquids, including certain injectable solutions and pharmaceutical preparations. It can also be suitable for products containing antimicrobial substances, provided the filtration and rinsing procedures adequately address potential microbial inhibition.
2. Direct Inoculation Method
Direct inoculation involves transferring a specified quantity of the product directly into suitable culture media.
The inoculated media are then incubated under controlled conditions to determine whether microbial growth occurs. Different media are used to support the detection of aerobic and anaerobic bacteria, as well as fungi.
This approach is generally appropriate for products that cannot be processed through membrane filtration, including certain ointments, creams, and medical devices.
The main consideration is ensuring that the product itself does not inhibit microbial growth, as this could produce misleading negative results.
The Sterility Testing Procedure: Step by Step
Although specific procedures vary depending on the product and applicable regulatory standards, sterility testing generally follows several stages:
- Sample preparation: Representative samples are collected and prepared under controlled conditions to prevent external contamination.
- Method selection: The laboratory determines whether membrane filtration or direct inoculation is appropriate for the product.
- Inoculation: The sample is introduced into suitable culture media using the selected testing method.
- Incubation: The culture media are maintained under specified conditions for the required incubation period, typically 14 days under USP 71 procedures.
- Observation: Laboratory personnel examine the media for signs of microbial growth throughout the testing period.
- Result interpretation: The results are evaluated according to the applicable pharmacopeial requirements, with any observed growth investigated as appropriate.
A test showing no microbial growth is generally interpreted as meeting the sterility test acceptance criteria. However, any positive result requires careful investigation to determine whether it reflects genuine product contamination or an issue with the testing procedure.
Applications of Sterility Testing
Sterility testing is used across several industries where microbial contamination can create significant safety risks.
Pharmaceutical manufacturing: Injectable drugs, intravenous solutions, vaccines, and ophthalmic products undergo sterility testing to support microbiological quality assurance.
Medical devices: Products such as surgical instruments, implants, catheters, and other devices intended for sterile use require appropriate sterility assurance and testing.
Biotechnology: Certain biological products, cell-based therapies, and specialized pharmaceutical preparations require sterility testing as part of their quality control processes.
Healthcare and laboratory environments: Sterility testing also supports the evaluation of selected sterile materials and preparations used in medical and laboratory applications.
Final Thoughts
Sterility testing is an essential component of pharmaceutical and medical quality assurance. By identifying potential microbial contamination, manufacturers can better protect patients, maintain product integrity, and demonstrate compliance with established regulatory standards.
Choosing the appropriate testing method, following validated procedures, and maintaining controlled laboratory environments are all important for obtaining reliable results. Combined with effective sterilization validation and contamination-control strategies, sterility testing helps ensure that products intended for sterile applications meet the required standards before reaching end users.
About the Author